INK PRODUCTION SOLUTION

Ink Production Solutions: Dispersion and Wet Grinding

A POLYC ink production line combines powder induction and pre-dispersion, horizontal bead milling, letdown, filtration and filling. Inline dispersion can reduce milling time by about two-thirds and energy use by more than half, with reference throughput around 1,200 kg/h for NC white ink at about 40% pigment loading.

A practical guide to ink production using inline dispersion, horizontal bead milling, blending, filtration and filling equipment.

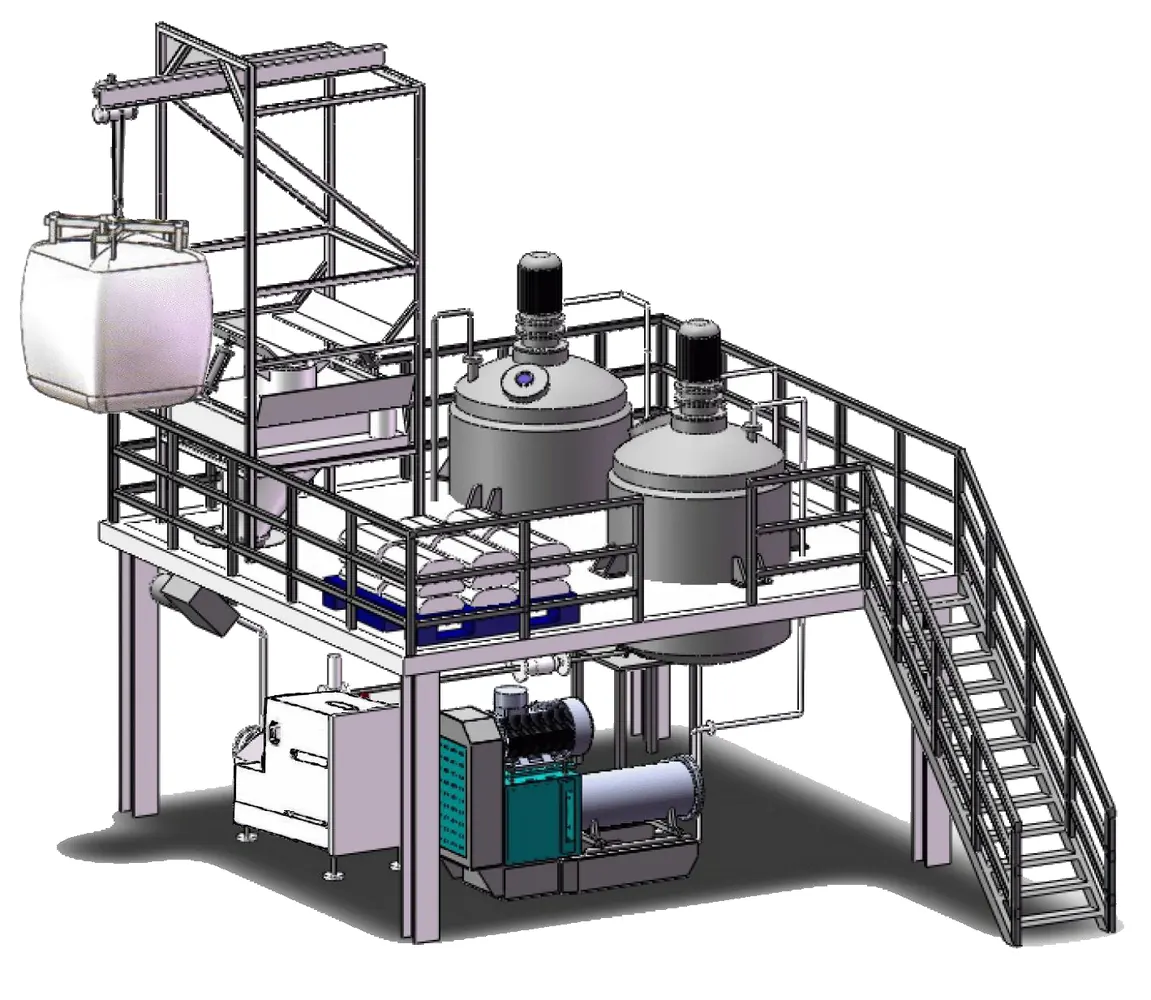
Integrated ink production process layout
01

A complete ink production workflow

A production line normally combines liquid dosing, powder handling, pre-dispersion, wet grinding, letdown, filtration and filling. Each stage should be sized around pigment loading, binder system, viscosity, target fineness and batch frequency.

  • Controlled dosing and weighing
  • Dust-controlled pigment induction and wetting
  • Bead milling to the required particle-size distribution
  • Final blending, filtration and filling
02

Traditional and integrated process routes

A conventional route uses a high-speed disperser before a vertical or horizontal bead mill. An integrated route can use an inline dispersion machine to induct, wet and de-agglomerate powder before horizontal bead milling, reducing the load on the grinding stage.

  • Conventional: vessel charging, Cowles dispersion, bead milling, letdown
  • Integrated: inline powder induction, circulation dispersion, bead milling, letdown
  • The preferred route depends on powder behavior, solvent safety, cleaning frequency and throughput
03

How inline dispersion works

High liquid velocity creates a controlled vacuum for powder induction. The rotor-stator zone increases liquid surface area, wets powder rapidly and circulates the mixture for dispersion and de-agglomeration. A closed arrangement can reduce airborne dust and manual powder handling.

  • Powder induction and wetting in one circulation loop
  • Configurable tank volume, drive power and cooling
  • Suitable controls selected for water-based or solvent-based formulations
04

Selecting the grinding stage

Disc bead mills are commonly selected for productive micron-scale grinding. Pin-type bead mills provide higher grinding intensity when narrow particle-size distribution or nano-scale targets are required. Mill volume, media size, tip speed, cooling and pass strategy must be confirmed by formulation.

  • Disc mill: coatings, gravure ink, flexographic ink and pigment dispersions
  • Pin mill: inkjet ink, automotive coatings, carbon black paste and advanced dispersions
  • Basket mill: flexible batch production and frequent color changes
05

Information needed for engineering

For equipment selection, provide the liquid system, pigment type, solids content, viscosity, feed size, target fineness, batch size, hourly capacity, temperature limit and hazardous-area requirements. These inputs determine the process route and equipment configuration.

  • Material safety and solvent information
  • Batch or continuous production preference
  • Cleaning and product-change requirements
  • Utilities, layout and automation scope
06

Ink types and printing processes

Ink formulations cover liquid inks (gravure, flexographic, news ink) and paste inks (offset, screen, UV). The choice between water-based, solvent-based or UV chemistry affects drying, viscosity, pigment loading and the required grinding intensity.

  • Gravure inks: solvent-based (toluene, EAC) or water-based, used for packaging and labels
  • Flexographic inks: UV, solvent or water-based, used for flexible packaging and food contact
  • Offset inks: high-viscosity paste, often requiring three-roll mills rather than bead mills
  • UV and energy-curable inks: low-volatility, often need cooling during grinding
07

Horizontal vs vertical bead mill comparison

Horizontal bead mills distribute grinding media evenly and can load up to 80% of chamber volume. Traditional vertical mills suffer from gravity settlement of media, lower media loading and lower energy density.

AspectHorizontal Bead MillVertical Bead Mill
Media distributionEvenly distributed, no gravity settlementBeads sink by gravity, uneven density
Media loadingUp to 80% of chamber volumeLower loading volume
Peripheral speedUp to 13-16 m/sAround 10 m/s
Energy densityHigh (Pv > 2 kW/L)Low
FinenessNano and sub-micron achievableGeneral micron only
PSDNarrow distributionBroad distribution
Capacity examplePZP30: up to 500 kg/h for white/yellowSlower throughput
    08

    IDS inline dispersion: measured results

    Inline dispersion improves pigment wetting and de-agglomeration, typically reducing milling time by two-thirds and cutting energy use by over 50%. In a TiO2 water-based trial at 55% solids and 45 deg C limit, the particle-size distribution after induction and 15-minute circulation reached the following values:

    D03D06D10D16D25D50D75D84D90D97
    0.085 um0.092 um0.101 um0.115 um0.153 um0.224 um0.295 um0.344 um0.421 um0.987 um
    • NC gravure inks: fineness below 1.25 um in production
    • Automotive plastic paint: one line saves ~215 kWh per day
    • Emulsion paint (5 m line): saves ~348 kWh per day
    • Dust-free powder induction reduces manual handling and solvent exposure
    09

    PZP disc-type bead mill models

    The PZP series covers laboratory to production sizes for 5-10 micron applications such as architectural coatings, gravure inks, flexographic inks and pigment dispersions.

    ModelVolume (L)Motor Power (kW)Peripheral Speed (m/s)
    PZP11411.3
    PZB567.512.5
    PZB10101113
    PZB20202213
    PZB303030/3713
    PZB60607514
    PZB15015016014
    • Disc materials: wear-resistant alloy (standard), tungsten carbide, ZrO2 ceramic, or PU
    • Chamber materials: wear-resistant steel (standard), high-nickel alloy, SiC ceramic, or PU
    10

    PZB pin-type bead mill models

    The PZB pin-type series delivers higher grinding intensity for nano-fineness applications such as inkjet ink, automotive paint, carbon black paste and battery slurries.

    ModelVolume (L)Motor Power (kW)Peripheral Speed (m/s)
    PZB215.512
    PZB661514
    PZB10102214
    PZB20203014
    PZB30304514
    PZB60607515
    PZB15015016016
    • Fineness down to 200 nm with narrow particle-size distribution
    • Agitator cooling combined with chamber cooling for heat-sensitive products
    11

    Reference route: NC white ink

    A reference NC white ink route combines an IDS inline dispersion machine with a PZP disc bead mill. Solvent and varnish are charged first; TiO2 is inducted powder-side at high rate, wetted and circulated before fine grinding.

    • IDS inline dispersion for dust-free TiO2 induction and rapid wet-out
    • PZP30 disc bead mill for fine grinding; white ink can reach target fineness in one pass
    • CMYK and other colors typically require recirculation rather than a single pass
    • Reference throughput: around 1200 kg/h for white ink at about 40% pigment loading
    • Solvent set: IPA, EAC and ester/aromatic solvents matched to the resin system
    12

    Measured energy savings with inline dispersion

    Inline powder induction replaces manual powder handling and a separate Cowles pre-mix loop. In production references it has cut milling time by about two-thirds and reduced energy use by more than half.

    • Automotive plastic paint line (~2400 L/day): about 215 kWh saved per day, roughly 64,000 kWh per year
    • Emulsion paint line (about 5 m batch, ~8500 kg): about 348 kWh saved per day, roughly 104,000 kWh per year
    • Dust-free induction also reduces manual powder handling and airborne solvent exposure
    • Actual savings depend on formulation, batch size and the existing equipment being replaced
    13

    Why the PZP disc mill design is efficient

    The PZP disc mill uses reverse-feeding agitator discs and a turbo discharge separation that keeps grinding beads away from the screen. This allows smaller media and a larger open screen area for high flow at low chamber pressure.

    • Reverse-feeding beveled discs scatter beads evenly and avoid bead compression
    • Turbo discharge separates beads without hydraulic compression at the outlet
    • Large screen surface lowers chamber pressure and limits temperature rise
    • Productive family from a 1 L lab unit up to a 150 L production mill
    14

    Why the PZB pin mill gives strong color strength

    Pin-type mills run higher energy density and accept smaller media for narrow particle-size distributions. Combined chamber and inner-rotor cooling keeps temperature even, which supports a narrow PSD and stronger color strength at lower pigment loadings.

    • Grinding intensity reaches into the nano range, down to about 200 nm
    • Centrifugal separation allows small beads without screen blinding
    • Chamber cooling plus agitator rotor cooling prevents product overheating
    • A narrow PSD means more uniform shade and less pigment needed in the final product
    15

    Choosing the right mill for your ink

    Select equipment based on target fineness, viscosity and batch frequency. Basket mills suit flexible color changes; disc mills are the workhorse for micron-scale production; pin mills are needed when nano fineness or narrow PSD is required.

    • 10-20 um: basket mill or disc-type horizontal mill
    • 5-10 um: disc-type horizontal bead mill (coatings, gravure, flexo)
    • Nano / sub-micron: pin-type bead mill (inkjet, automotive, carbon black)
    • High-viscosity paste (offset ink): three-roll mill
    • Flexo white/yellow reference: PZP30 around 500 kg/h in about 2 passes
    • Flexo black reference: around 350-400 kg/h in 3-4 passes
    16

    Ink line at a glance

    The grinding stage follows the ink chemistry rather than the machine catalogue. The table below summarises the usual match between ink type, viscosity and target fineness, using the references described on this page.

    Ink typeTypical viscosityFineness targetRecommended grinding stage
    Gravure, solvent or water-basedLowBelow 5 microns in production; NC gravure below 1.25 microns in reference trialsDisc bead mill or pin mill
    Flexographic, solvent, water or UVLow to mediumBelow 5 micronsDisc bead mill
    Inkjet and digitalLowD90 below 200 nmPin-type nano bead mill
    Offset pasteHighControlled by three-roll gapThree-roll mill rather than a bead mill
      17

      Quality checks on an ink line

      Ink quality is decided long before the filling head. The checks below are normally applied at the stages shown, and each result should be recorded against the batch so that a drift is visible before a customer sees it. The Ethiopia gravure ink project is a worked example of the same sequence on a 200-300 kg/h line.

      CheckMethodStage
      Fineness of grindHegman gauge or particle-size analyserAfter milling
      Particle size distributionLaser diffraction, reported as D50 and D90After milling and at letdown
      ViscosityRotational viscometer at working temperatureAfter letdown, before filtration
      Colour strengthDrawdown against a retained reference standardAfter letdown
      Filtration integrityInspection of bag or cartridge filter after the batchBefore filling
      • Compare samples at equal temperature, never hot against cold
      • Retain a reference drawdown for every approved batch
      • Record mill flow, tip speed and cooling data alongside the result

      Production stages in detail

      Pre-dispersion

      Liquids are charged first before pigments and additives are introduced under controlled shear. The objective is complete wetting without dry pockets, excessive air entrainment or a viscosity peak that prevents stable transfer to the mill.

      Wet grinding

      The mill reduces agglomerates under controlled media loading, flow, speed and cooling. Samples should be compared at equal temperature using the same particle-size or fineness method before throughput is increased.

      Letdown & filtration

      Resin, solvent, water or additives are adjusted in the finishing vessel. Final viscosity, shade and solids are confirmed before filtration removes oversized contamination and the product moves to filling.

      Grinding equipment options

      Disc bead mills

      A disc mill supports productive continuous grinding for gravure, flexographic and general industrial inks where stable micron-scale quality and high circulation flow are required.

      Pin type bead mills

      A pin rotor creates higher grinding intensity and accepts smaller media for narrow particle-size distributions in inkjet, automotive, carbon-black and other fine dispersions.

      Basket mills

      A basket mill combines dispersion and grinding in one batch vessel. It suits frequent color changes, flexible batch sizes and plants that prioritize straightforward cleaning.

      Typical ink formulation and equipment selection

      The formulation route determines materials, safety controls and the preferred grinding system.

      Ink typeProcess characteristicsTypical equipment routeKey review point
      Solvent-based inkResin solution, organic solvent and pigmentClosed disperser + horizontal bead mill + filterHazardous-area classification and seal compatibility
      Water-based inkWater, resin or emulsion, pigment and additivesInline or high-speed disperser + disc bead millFoam control, corrosion and microbial management
      UV inkReactive oligomer, monomer, pigment and photoinitiatorTemperature-controlled pre-mixing + pin bead millHeat exposure, viscosity and light protection

      Capacity and fineness reference

      These are preliminary engineering ranges, not guaranteed results. Material trials determine the final selection.

      Equipment exampleOperating modeIndicative production referenceTypical quality objective
      1000 L basket mill systemBatch500-1000 L working batch; evaluate roughly 45-120 minutesApproximately 5-20 micrometres
      20-30 L horizontal disc millContinuous or circulationApproximately 100-600 L/h depending on formulationApproximately 5-10 micrometres
      20-30 L pin bead millContinuous or circulationApproximately 40-250 L/h depending on viscosityFine micron to submicron range

      Quality control at each stage

      Use a calibrated fineness gauge for routine production checks and particle-size analysis when a distribution target is specified. Record sample temperature because viscosity and apparent fineness can change as the batch warms.

      Viscosity must be measured with an agreed spindle, speed and temperature. Shade, color strength, gloss, solids and density should be checked against the approved method. Final filter rating is selected against pigment size, product viscosity and filling requirements rather than chosen as a universal value.

      A useful production record connects raw-material lots, charging order, dispersion time, mill settings, sample results, filtration pressure and accepted output. This makes formulation variation distinguishable from wear, cooling or operating changes.

      Common problems and corrective actions

      Uneven dispersion often begins with poor wetting, an unstable feed viscosity or powder charging faster than the liquid can accept it. Low grinding efficiency can result from unsuitable media size, low media loading, excessive flow, worn agitators or inadequate cooling. Foam is addressed by reducing air entrainment, reviewing pump return position, controlling shear and confirming that any defoamer is compatible with the formulation.

      Change one operating variable at a time and sample consistently. Increasing speed or extending time without confirming temperature, viscosity and media behavior can consume more energy without improving saleable product quality.

      FROM THE PRESENTATION

      Process and equipment highlights.

      Inline dispersion machine powder induction principle
      Inline powder induction and liquid circulation principle
      Pigment agglomerate dispersion illustration
      Pigment wetting and de-agglomeration
      Ink particle size distribution chart
      Particle-size distribution evaluation after dispersion
      POLYC disc type horizontal bead mill
      Disc-type horizontal bead mill
      POLYC pin type nano bead mill
      Pin-type bead mill for fine and nano grinding
      Ink production equipment arrangement
      Integrated equipment arrangement for ink production
      Flexographic white ink IDS plus PZP30 single-pass process flow
      Flexo white ink route: powder dosing, IDS inline dispersion, PZP30 grinding, letdown and filtration
      Ink production line engineering sketch with dosing, inline dispersion and pin mill
      Line sketch: dosing station, IDS inline disperser, PZP pin mill and bag filter
      Big-bag dust-free powder dosing station with inline dispersion
      Dust-free big-bag powder dosing station feeding an inline dispersion machine
      POLYC basket mill for batch dispersion and grinding
      Basket mill for flexible batches and frequent color changes
      POLYC horizontal bead mill for wet grinding
      Horizontal bead mill with process piping and instrumentation
      PZP disc type bead mill rotor and discharge assembly
      PZP disc-type rotor and turbo discharge separation assembly
      PZP reverse-feeding beveled grinding discs close up
      Reverse-feeding beveled discs scatter beads evenly and avoid bead compression

      RELATED EQUIPMENT

      Explore the equipment in this presentation.

      IDS Inline Dispersion Machine

      The IDS Inline Dispersion Machine is a dust-free, continuous in-line disperser that rapidly mixes and disperses solids and liquids using a rotor-stato

      View equipment →

      High Efficiency Static Disc Bead Mill

      Static disc bead mill for ultrafine grinding, supporting media down to 0.1mm with static centrifugal discharge.

      View equipment →

      Pin Type Bead Mill

      Horizontal pin-type bead mill for nanometer-range grinding, supporting media down to 0.2mm with centrifugal separation and force cooling.

      View equipment →

      Ink Production Line

      Ink Production Line: Semi-Automatic or Fully Automatic, Built to Your Capacity

      View equipment →

      FREQUENTLY ASKED QUESTIONS

      Questions about this presentation.

      What equipment is needed for ink production?

      A typical line combines pre-dispersion, bead milling, letdown, filtration and filling. The exact route depends on the ink chemistry, viscosity, target fineness and production mode.

      Bead mill vs basket mill for ink?

      Choose a horizontal bead mill for continuous production and stable high throughput. Choose a basket mill for flexible batches, frequent color changes and simpler cleaning.

      What grinding media is used for ink?

      Zirconia media in approximately the 0.3-1.0 mm range is common, but media size and density must match the mill, pigment, feed size and target fineness.

      How can dispersion efficiency be improved?

      Prepare a stable pre-dispersion, control slurry viscosity and temperature, select suitable media loading and maintain consistent flow. Inline powder induction can improve wetting before milling.

      What fineness should an ink line target?

      It depends on the printing process. Gravure and flexographic inks are commonly specified below 5 microns, while NC gravure references reach below 1.25 microns in production. Inkjet and digital inks require sub-micron grinding, typically D90 below 200 nm, which is why a pin-type nano bead mill is used.

      How is viscosity adjusted after grinding?

      In the letdown or finishing vessel, resin, solvent, water and additives are adjusted until the specified viscosity and solids content are reached. Viscosity is measured at working temperature before filtration, because a reading taken hot will not match the customer specification.

      Can one line run solvent-based and water-based inks?

      The mechanical arrangement can be similar, but the electrical and sealing specification is not. Solvent-based inks require explosion-proof motors and controls, solvent-resistant seals and appropriate ventilation, and cleaning between chemistries must be planned into changeover.

      What throughput can an ink line reach?

      Throughput follows the ink type and pigment loading. In the reference route described on this page, NC white ink runs at around 1,200 kg/h at about 40% pigment loading, while a small-batch gravure line may be sized for 200-300 kg/h. Both figures depend on the target fineness and the number of passes.

      How is colour strength kept consistent?

      Consistency comes from controlled pigment dispersion, a stable particle-size distribution, weighed letdown additions and a retained reference drawdown. Recording mill parameters with each batch makes a drift traceable to a specific stage rather than to the finished product.

      What is the difference between single-pass and recirculation grinding?

      White ink can often reach target fineness in a single pass through a disc bead mill, which suits high-volume production. CMYK and other colours typically require recirculation, trading throughput for a narrower particle-size distribution and lower peak temperature.

      DISCUSS YOUR PROCESS

      Turn the presentation into a practical equipment plan.

      Share your material, capacity and quality targets with the POLYC MACHINE engineering team.

      Talk to an engineer →
      Get a Quote →WhatsApp
      Chat on WhatsApp